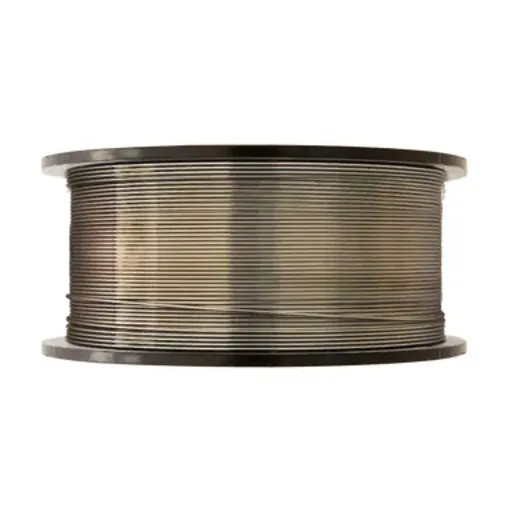
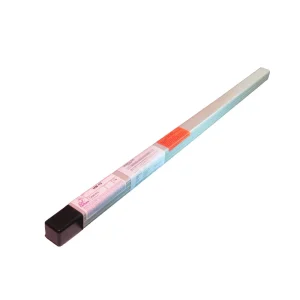
E81T1-B2 Wire – 0.045 in – 33 lb
A titania slag formulation flux cored wire for single or multi-pass welds on 1.25% Cr 0.5% Mo steels
The weld deposits are designed to operate at high temperature service. The shield gas recommended is 100% CO2
A preheat of 200-350°C and a post-weld heat treatment of 680-730°C for 1 hour per inch of thickness followed by air cooling to ambient temperature is required
Features
- A titania slag formulation flux cored wire for single or multi-pass welds on 1.25% Cr 0.5% Mo steels
- The weld deposits are designed to operate at high temperature service. The shield gas recommended is 100% CO2.
- A preheat of 200-350°C and a post-weld heat treatment of 680-730°C for 1 hour per inch of thickness followed by air cooling to ambient temperature is required
- For use with high pressure vessels, oil refining industries, steam pipes of boilers
- This wire is designed for welding of 1.25% Cr-0.5% Mo steel used for high pressure vessels, oil refining industries, steam pipes of boilers etc.
- It is a rutile type flux cored wire for all position welding.
- It provides smooth arc, low spatter levels, good weldability, and good bead appearance.
- The weld metal contains about 1.25% Cr. 0.5% Mo, so it has good crack and heat resistance.