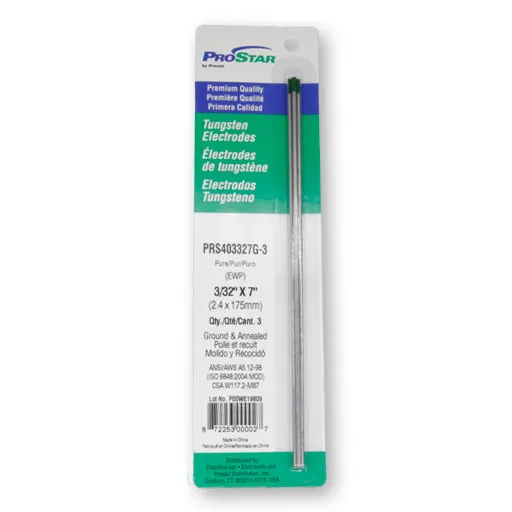
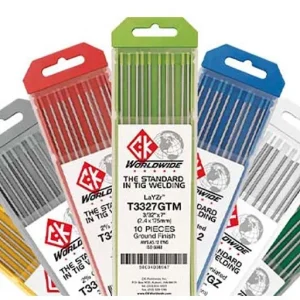
ProStar Tungsten Electrodes, 5/32″?7″
Quality Tungsten Electrodes
•Pure Minimum 99.5% tungsten is used mainly with alternating current (AC) for welding aluminum and magnesium alloys. AC current causes the electrode to form a clean, balled end. Pure tungsten is more prone to contamination of the weld than other types of tungsten. It may be used as a shielding gas with direct current (DC), with Ar, He, or a mixture of both.
1.5% Lanthanated Non-radioactive. Best for use in direct current (DC). Best for noncorroding steels, titanium, nickel, and copper alloys. Good arc starts and stability; low erosion rate with a wide amperage range.
2% Lanthanated Non-radioactive. Good general-purpose electrode for both alternating current (AC) or direct current (DC). Recommended for low-alloyed and noncorroding steels, aluminum, magnesium, titanium, nickel, and copper alloys.
2% Ceriated Non-radioactive. Best when used with alternating current (AC) on aluminum and magnesium alloys. Balls easily provide improved arc stability and ease of starting.
ZirConiated Best for use with Alternating Current (AC). Retains a balled end for welding aluminum and magnesium alloys and has a high resistance to contamination. Produces a stable arc. Not recommended for Direct Current (DC) applications.
ProStar’s Highest Quality Electrode
• Manufactured to comply with ISO9001 Certification
• Meets AWS/ANSI specifications
• Precision ground for maximum smoothness