They are either built into a MIG power source or separate units used with engine-driven welders and older power sources.
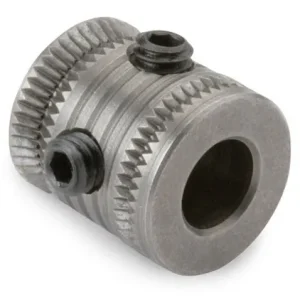
Feed speed range and drive roll configuration determine which wire sizes and types a feeder handles. Two-roll feeders suit light wire; four-roll feeders give more grip and are needed for soft wires like aluminium and for long gun lengths. Drive roll groove profile must match the wire — V-groove for solid wire, U-groove for softer wires, knurled for flux-cored.
Voltage-sensing (or across-the-arc) feeders work with constant-current power sources, which is how engine-driven welders run MIG. Constant-voltage feeders need a CV power source. Mixing the two types gives poor arc characteristics rather than no arc at all, which makes the mistake easy to miss.
Spool capacity and mounting determine how often the wire is changed. A 10 lb spool suits occasional work; 33 and 44 lb spools are the production standard.
