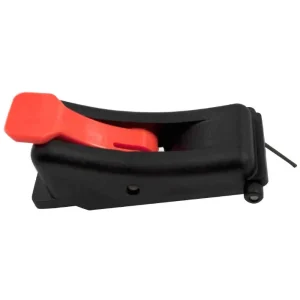
Torch selection is driven by cutting amperage, by whether the work is hand-held or machine-mounted, and by the type of cutting being done.
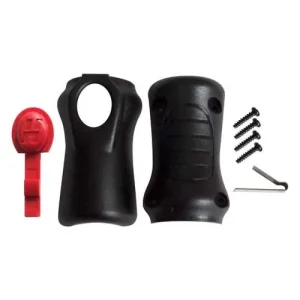
Hand torches are shielded for dragging along the plate, with a standoff guide that keeps the nozzle at the right height. Machine torches mount rigidly on a table or CNC carriage and hold a fixed standoff, which gives more consistent cut quality but no flexibility in angle.
Cutting amperage sets the maximum material thickness. A torch rated to 45 A will sever about 1/2 in steel; 85 A reaches around 3/4 in; 105 A and above handle 1 in and thicker on a machine torch. Exceeding the rated thickness produces dross and a rough edge rather than a clean cut.
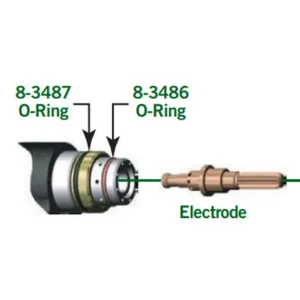
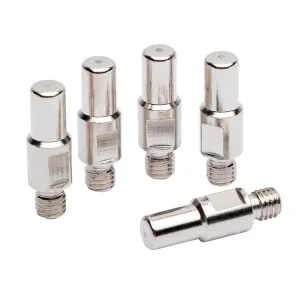
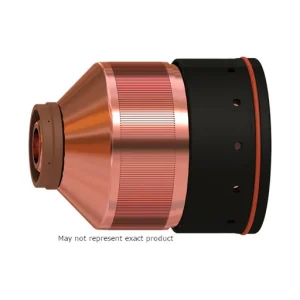
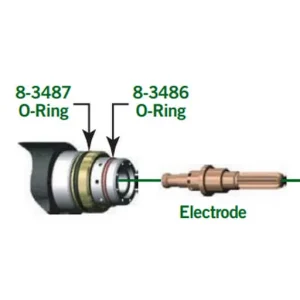
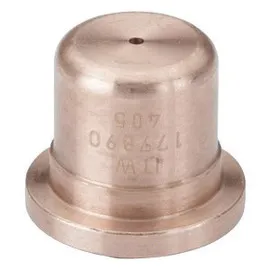
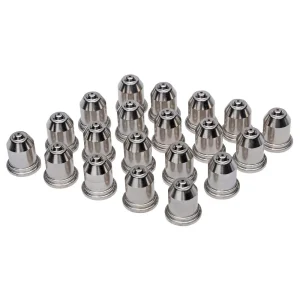
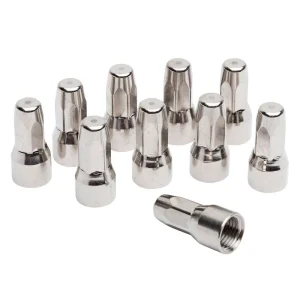
Consumables are torch-specific and amperage-specific. The same torch family uses different electrode and nozzle sets for different amperages and for cutting versus gouging, so the wrong set will either not fit or will cut badly.
