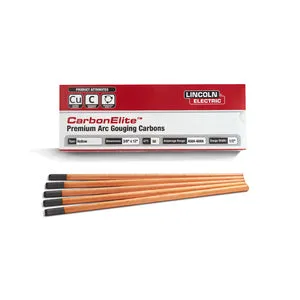
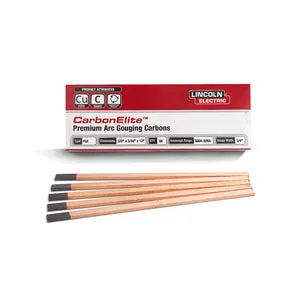
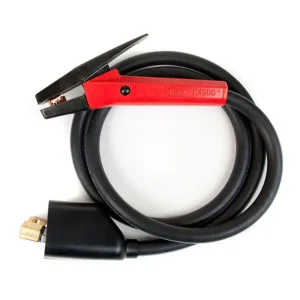
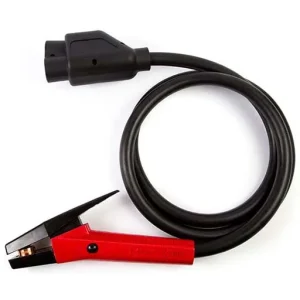
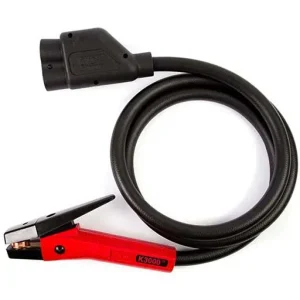
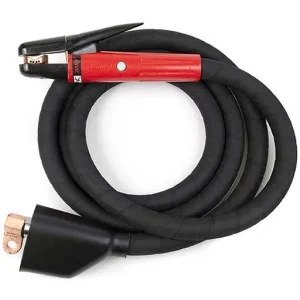
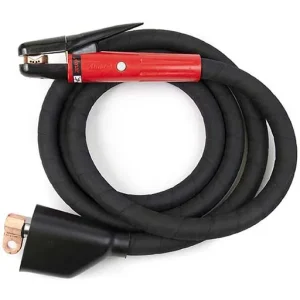
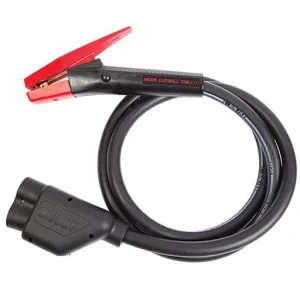
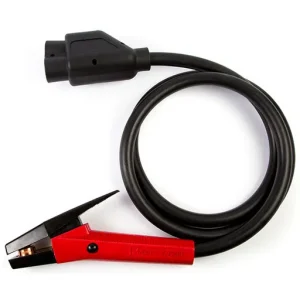
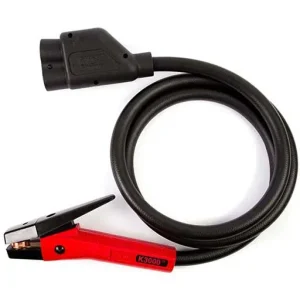
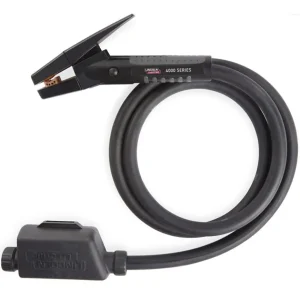
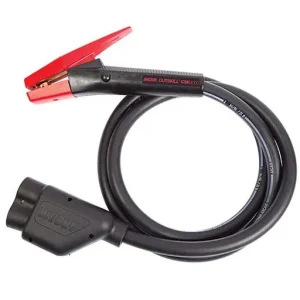
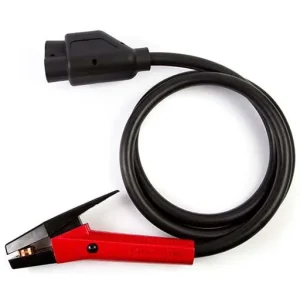
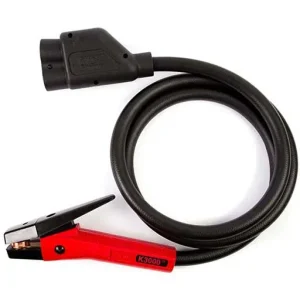
It is the standard method for back-gouging weld roots, removing cracks and old welds, and preparing joints.
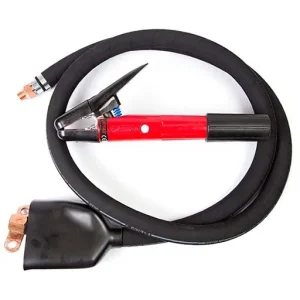
Gouging requires a constant-current power source with enough amperage for the electrode size — typically 200 to 400 A and above. A MIG or CV power source will not gouge properly. The compressed air supply must be dry and at sufficient pressure, usually 80-100 psi, delivered through a gouging torch with the air jets correctly aligned behind the electrode.
Carbon electrodes are copper-coated for conductivity and are sized by diameter, which sets the groove width. Pointed electrodes gouge narrow, deep grooves; flat or jointed electrodes gouge wide, shallow ones. Electrode consumption is high and the process produces a lot of smoke and spatter, so fume extraction and PPE are essential.
